ELECDURA NETWORK

Your Whole New Supply Chain For Heavy-Duty Parts
Whatsapp:
+86 18915027366
Phone:
+86 18915027366
Views: 0 Author: Site Editor Publish Time: 2026-08-19 Origin: Site
A heavy-duty alternator can show weak output, intermittent excitation, unstable charging, or excessive brush wear even when the stator and rectifier are serviceable. The fault may sit in the rotor field winding, a slip-ring lead, the insulation path, an eccentric ring, a contaminated surface, or the brush-to-ring interface.
Resistance alone is not a universal pass value. Copper changes with temperature, test leads add error, and different rotor families use different winding designs. A rebuild decision therefore needs identity, temperature, geometry, insulation, surface condition, and field-current evidence tied to the exact alternator reference. Buyers can use the Elecdura alternator category to organize reference and application research while the workshop keeps measured evidence in control of the final decision.
This guide helps rebuilders, fleet workshops and wholesale buyers specify evidence for a confirmed brush-type unit. It does not supply universal resistance, insulation-test voltage, machining or excitation limits. Qualified personnel must use the exact manufacturer procedure and a safe, isolated test setup.
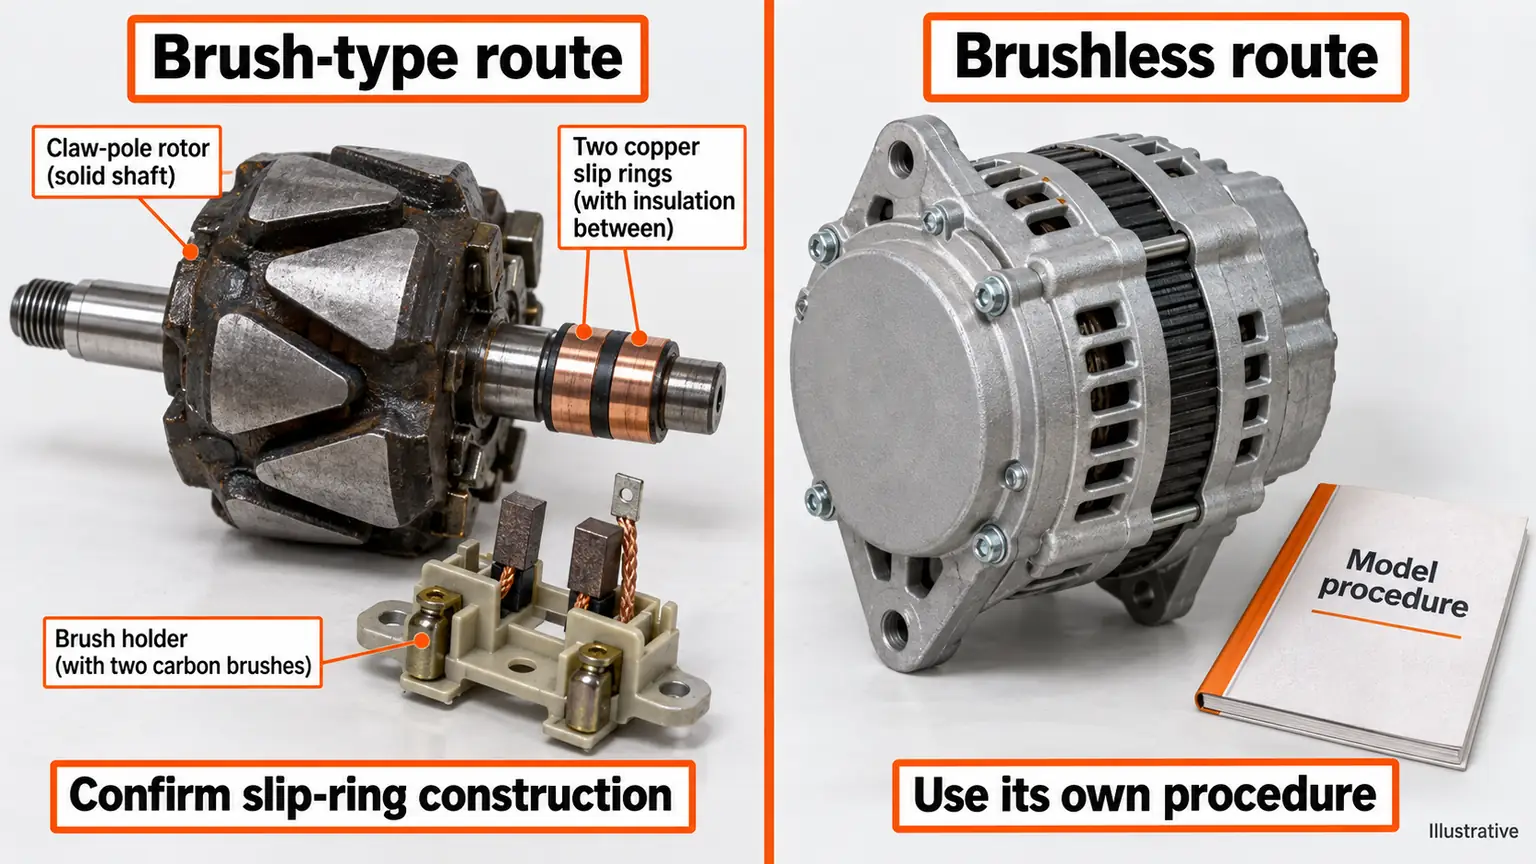
This guide applies to a brush-type alternator with a rotor field winding connected through slip rings. Confirm the exact internal construction before choosing measurements. Delco Remy identifies the 40SI and 55SI as brushless families: ring-to-ring resistance, brush length and brush-contact voltage-drop checks below are not their acceptance tests. Use the exact brushless model's service procedure instead. An aftermarket cross-reference or a similar housing does not establish internal construction.
Illustrative architecture distinction, not model identification from appearance. The brush-type example is not a 40SI or 55SI; confirm actual construction and the exact service instructions.
The manufacturer's brushless design information explains this architecture distinction. It is the reason for excluding those examples, not an approval of any replacement product shown here.
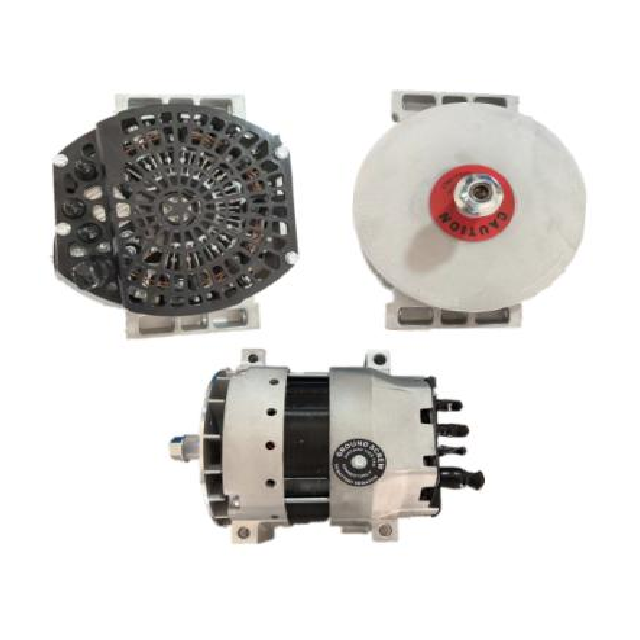
Architecture exclusion example: this catalogue image is associated with a 55SI reference. The OEM 55SI family is brushless. The photograph does not show an accessible brush-type rotor or demonstrate any test in this guide; verify the actual supplied unit separately.
If the assembly is brushless, or its construction is not established, stop this slip-ring route and obtain the correct procedure. The absence of accessible rings is not evidence of an open winding. For a confirmed brush-type unit, record alternator family, voltage, rated output, regulator strategy, pulley, rotor reference, ambient temperature and winding temperature before measuring. Before testing, the fleet electrician ties alternator and rotor reference to a named vehicle, engine, or bench configuration. That baseline gives field-winding resistance, temperature correction, ground insulation, slip-ring geometry, brush interface, and controlled rotor release a measurable starting point and prevents a convenient no-load observation from defining the entire alternator case.
Establish alternator and rotor reference first, then compare field-terminal layout while the original complaint is reproduced. Use winding temperature to challenge the first interpretation and retain service-limit source as the condition that another workshop or supplier can repeat. Temperature, speed, load, connection point, and instrument identity belong beside every value.
The opening record must explain why alternator and rotor reference represents the starting state and how field-terminal layout changes when the suspected failure appears. If winding temperature points elsewhere, the diagnosis stays open. service-limit source becomes the reference used to compare the removed unit, approved sample, and later production lot.
alternator and rotor reference: capture the initial value and the exact operating condition.
field-terminal layout: compare the response before and during the complaint.
winding temperature: use an independent observation to test the first theory.
service-limit source: preserve the reference with date, instrument, and reviewer.
A resistance result is meaningful only when it is compared with the correct rotor specification at a known temperature. A missing baseline cannot be recreated from memory after replacement, so unresolved fields remain marked pending. The first gate closes only when the complaint and the recorded alternator behavior describe the same event.
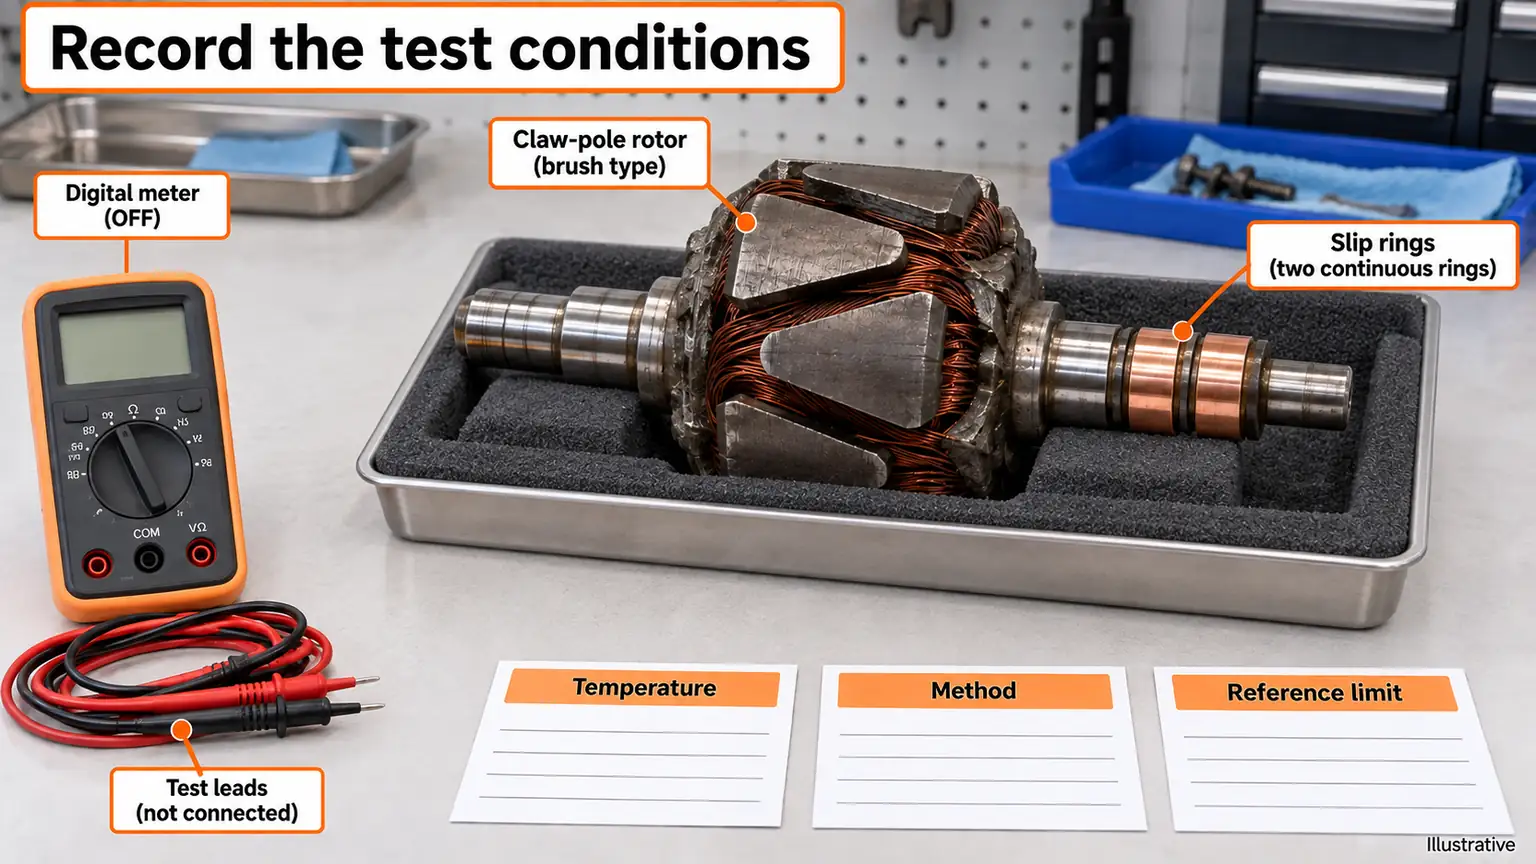
Illustrative evidence-review context, not a connected test or measured result. Use the specified method, temperature basis and exact rotor limit; no universal resistance or insulation-test setting is implied.
Confirm that the documented construction and service reference match the actual unit before selecting a test. Keep an unknown architecture on hold; an identity check does not itself approve fitment or a purchase.
Use compensated leads or a four-wire method where appropriate, stable contact pressure, clean probe points, and repeated readings around the ring circumference. This stage converts the initial observation into a controlled test route. The bench technician prepares lead compensation, verifies the connection or mechanical setup, and records the ambient and starting condition before applying a load, command, or movement.
Measure ring-to-ring resistance at the first defined point, then recheck repeatability after the alternator reaches the second condition. temperature correction should reveal whether the change follows the component, the host system, or the test setup. A changed cable, adapter, fixture, or speed invalidates the comparison unless it is documented.
For measure field-winding resistance across the slip rings, the test sheet should let a second technician rebuild the same arrangement. It identifies the fixture, probe locations, timing, units, applied demand, and the reason each reading matters to the suspected failure.
lead compensation: define the pre-test state and preparation method.
ring-to-ring resistance: log the first controlled response with its unit and tolerance.
repeatability: repeat at the second condition without changing unrelated variables.
temperature correction: note the deciding observation and any remaining ambiguity.
An open reading may come from the winding or a slip-ring lead, while an unexpectedly low value can indicate shorted turns or an incorrect rotor family. If the two controlled points do not support one explanation, return to the setup instead of forcing a conclusion. Release requires a repeatable route, not a single favorable reading.
Close measure field-winding resistance across the slip rings only after the setup can be rebuilt from the recorded fixture, connection, load, timing, and instrument details. The result advances diagnosis but does not waive later batch controls.
Apply only the approved insulation-test method and voltage, then check each ring to the rotor shaft and magnetic structure while protecting connected electronics. The purpose here is pattern recognition rather than collection of isolated numbers. The receiving inspector aligns insulation resistance, test voltage, shaft ground path, and electronics isolation on one time line so the sequence of the alternator response remains visible.
Interpret insulation resistance only with the specified test voltage, isolation state, temperature and applicable service limit. Do not connect an insulation tester to the regulator or other electronics unless the exact procedure explicitly permits that arrangement. A changed setup must be documented before readings are compared.
A strong test rotor insulation to shaft and pole iron report saves raw traces or photographs before adding conclusions. The analyst labels normal features, suspected anomalies, and the point where the pattern changes, allowing a supplier to compare claim evidence with the approved sample.
insulation resistance: retain the unedited trace, image, or measured sequence.
test voltage: mark the feature that changes with the complaint.
shaft ground path: compare the same feature under a control condition.
electronics isolation: state which cause the combined pattern supports or excludes.
A rotor that carries field current but leaks to ground can create heat, regulator stress, unstable excitation, and repeat charging failures. When the pattern is incomplete, collect the missing operating interval instead of repeating the interpretation. The decision gate closes when the evidence sequence explains why the alternator changed.
Release test rotor insulation to shaft and pole iron when the saved pattern and control condition support one interpretation of the alternator behavior. Contradictory traces remain attached as open evidence.
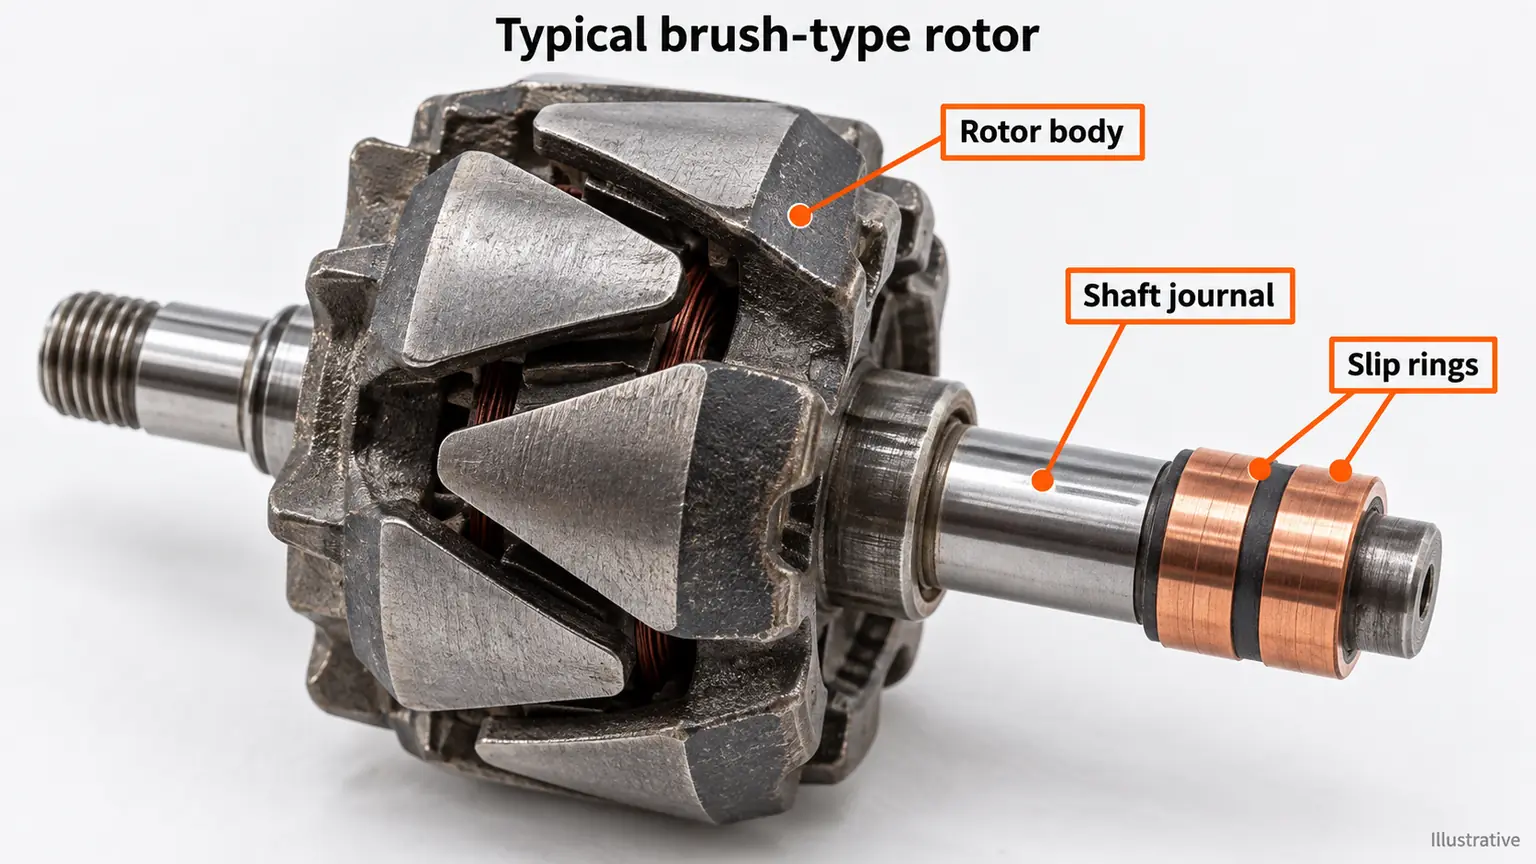
Measure diameter at several positions, radial runout on supported journals, groove depth, pitting, burning, contamination, solder joints, and ring security. This module examines how the alternator behaves after time, heat, load, or contamination has had an opportunity to act. The technical buyer defines the exposure interval and tracks minimum ring diameter before, during, and after that interval.
Illustrative typical brush-type rotor only, not a specific part, wear limit or machining instruction. Ring geometry and permissible service work must be checked against the exact rotor specification.
Correlate radial runout with surface finish rather than treating either value as a universal limit. Add lead-joint condition to show whether cooling, lubrication, sealing, supply, or surrounding hardware changed the result. The exposure must be long enough to reveal the complaint without exceeding the declared duty.
The inspect slip-ring diameter, runout, and surface worksheet should include ambient condition, starting temperature, applied duty, elapsed time, peak observation, stabilization point, and recovery behavior. These details distinguish a genuine stress-related defect from a test that simply overheated the assembly.
minimum ring diameter: establish the pre-exposure reference.
radial runout: capture the peak or worst-case behavior.
surface finish: compare the response at a fixed elapsed time.
lead-joint condition: document recovery and any permanent change.
A polished appearance does not prove that the rings are concentric, mechanically secure, or thick enough for another service cycle. A result outside the limit requires the surrounding system to be checked before the alternator is condemned. Approval waits until the stress route and recovery evidence agree.
Approve inspect slip-ring diameter, runout, and surface after exposure, peak response, stabilization, and recovery form one defensible sequence. The signature covers this stress route rather than unrelated endurance claims.
The 40SI listing belongs to a different, brushless-family application. Do not use its exterior photograph as evidence of slip-ring diameter, brush condition or an internal test point. For this section, use measurements and photographs of the actual verified brush-type rotor.
Inspect brush length, freedom in the holder, spring force, lead flexibility, contact pattern, polarity where relevant, and evidence of arcing or bounce. Bench inspection now tests the internal or component-level theory developed on the machine. The warranty analyst preserves the removed condition, cleans only what the method requires, and records brush projection before disassembly can erase useful evidence.
Quantify holder clearance with equipment suited to its expected range, verify spring force through a second method where practical, and photograph contact pattern beside the part identity. Compensation, temperature, fixture pressure, and zeroing matter when small differences drive the conclusion.
The bench record separates observation from interpretation. It states what was measured directly, what was inferred from the pattern, what limit was used, and whether that limit belongs to the exact alternator family under review.
brush projection: preserve the as-removed condition and reference marks.
holder clearance: record calibrated measurement and environmental correction.
spring force: confirm the suspected mechanism with a second observation.
contact pattern: connect visible condition with the measured failure path.
Rotor and brush findings must be evaluated together because a good winding can still receive unstable field current through a poor mechanical interface. If cleaning, dismantling, or fixture force could have changed the result, the report states that limitation. A batch decision must not rely on a bench value whose method cannot be reproduced.
Accept control brush contact and spring force when as-removed condition, calibrated values, compensations, and component photographs identify the same mechanism. Any destructive inspection limitation stays visible.
Use an approved regulator or test source to compare field current, rotor response, brush voltage drop, temperature rise, and intermittent behavior without overspeeding the assembly. Competing causes must now be separated so that the replacement addresses the failed section rather than the most visible symptom. The fleet electrician compares controlled field voltage and field current under the same demand before changing any component.
Use brush voltage loss to test the alternative explanation, then inspect thermal response for evidence that the host system created or amplified the complaint. Each branch needs a pass/fail reason; swapping parts until the symptom disappears does not identify the original alternator failure.
A cause map for evaluate field current under controlled excitation lists the evidence expected if each candidate fault were true. The actual readings are then placed against those expectations, including contradictory observations that prevent premature closure.
controlled field voltage: define what this result would mean for the primary theory.
field current: compare the alternative component or system response.
brush voltage loss: run the discriminating check that separates both paths.
thermal response: inspect the interface where one fault could imitate another.
Dynamic evidence can expose faults that disappear during a cold static ohmmeter check, especially at slip-ring joints and brush contacts. Replace the alternator only after the selected cause explains the complaint and the rejected cause fails its own evidence test. This gate protects the fleet from repeat failure and protects the supplier from an unsupported claim.
Pass evaluate field current under controlled excitation after the chosen cause explains the complaint and the competing cause fails its defined check. The signature prevents parts substitution from masquerading as diagnosis.
For the verified brush-type unit, reassemble only with the model-approved bearings, brush components, insulation, rectifier, regulator, pulley and fasteners. The brush requirement does not apply to brushless designs. Follow the applicable complete-alternator test procedure and record its specified cut-in, output, regulation, ripple and temperature checks. The final module converts technical findings into an acceptance standard that purchasing, receiving, and warranty teams can apply consistently. The bench technician defines how cut-in speed and hot-output curve will be compared between the approved sample and production units.
Add AC ripple to expose changes that a label or catalogue cross-reference cannot show. Use serial traceability to connect each result with the supplier lot, purchase order, and reviewer. Tolerances should reflect the actual heavy-duty duty cycle rather than an unspecified generic test.
The acceptance sheet for release the complete alternator with traceable results identifies mandatory evidence, sampling frequency, instruments, pass limits, quarantine action, and escalation owner. It also states which changes require a new sample or field trial.
cut-in speed: define the release value and sampling method.
hot-output curve: compare sample evidence with the incoming lot.
AC ripple: retain the technical record that exposes configuration drift.
serial traceability: trace approval, deviation, and claim decisions to one identity.
The rotor is approved only when component measurements and complete alternator performance agree under the recorded heavy-duty application. A production lot advances only when its evidence follows the approved route. Price, urgency, or stock shortage cannot silently waive a mandatory alternator acceptance field.
Authorize release the complete alternator with traceable results through a sampling plan, stated limits, traceable lot, quarantine rule, and deviation owner. Production release follows evidence rather than schedule pressure.
A defensible alternator case file links the complaint, operating duty, removed-part markings, test setup, raw readings, photographs, interpretation, and unresolved questions. For this diagnostic workflow, that record should also identify which evidence came from the vehicle, the bench, the supplier, and the receiving team so later decisions do not mix unlike sources.
Identify the alternator, host vehicle or machine, duty cycle, and original complaint.
Attach measurements that support the investigation described above without rewriting raw results.
Name the person who accepted each alternator limit and the person who owns each open question.
Connect the approved sample, purchase order, supplier lot, and incoming inspection record.
Technical diagnosis becomes commercially useful when an RFQ carries the same identity and limits. An alternator inquiry should include the original reference, engine or vehicle, photographs, measured interfaces, operating symptoms, tested conditions, required quantity, destination, and expected reorder frequency. This prevents a broad catalogue match from replacing the evidence developed above.
State whether the requested alternator is new aftermarket, remanufactured, or another declared condition.
List the actual mounting, pulley, electrical-terminal and regulator-interface requirements for this alternator.
Define sample evidence, receiving checks, packaging, labels, and change notification.
Keep price, MOQ, and lead time separate from unresolved technical fitment.
The approved alternator sample is useful only when its measurable configuration follows the purchase order into later shipments. Receiving should compare markings, connectors, mounting, visible construction, packaging, selected functional readings, and any promised documents. A changed configuration returns to technical review instead of entering fleet stock by habit.
Retain the approved alternator sample or a complete photo and measurement record.
Trace each incoming lot to the supplier declaration and purchase-order revision.
Quarantine a changed interface, label, internal reference, or test result.
Feed field failures back into the same evidence route used for initial approval.
Heavy-Duty Alternator Rotor Winding and Slip-Ring Testing works when every reading belongs to a defined condition and every decision belongs to a named owner. The result is a clearer root cause, a more precise aftermarket specification, and a receiving standard that can expose a change before it reaches a heavy-duty fleet.
Importers and fleet buyers can review Elecdura company information, send the completed evidence through the Elecdura alternator enquiry page, and use the Elecdura heavy-duty parts catalogue to connect the case with the appropriate product family. The quotation should answer the documented application rather than imply an unverified genuine or OE status.