ELECDURA NETWORK

Your Whole New Supply Chain For Heavy-Duty Parts
Whatsapp:
+86 18915027366
Phone:
+86 18915027366
Views: 0 Author: Site Editor Publish Time: 2026-07-31 Origin: Site
A failed injector copper washer allows combustion gas to escape past the injector seat. Early signs may be a rhythmic chuff, diesel odor, sticky black carbon, wet-looking residue, or unexplained correction values. Left in service, the leakage can erode the seat, seize the injector in the bore, damage the clamp interface, and contaminate nearby wiring.
Installing another washer without finding why the seal failed often produces a short-lived repair. Incorrect washer thickness, reused hardware, dirty seating faces, distorted clamps, excessive bore damage, and wrong torque procedure can all prevent uniform sealing. Distribution buyers can use the Elecdurauto fuel injector category to organize reference and installation case research while the workshop keeps measured bore test documentation in combustion-seal control of the final disposition choice.
This guide gives heavy-duty workshops, fleets, and parts distribution buyers a controlled method for diagnosis, removal, seat assessment, washer and hardware selection, installation, and post-repair verification.
Listen for combustion pulses and inspect odor, soot pattern, bubbling residue, cylinder balance, clamp area, and wiring contamination while avoiding assumptions based on black deposits alone. Before testing, the technical distribution nozzle buyer ties chuffing sound to a named vehicle, engine, or bench injector-seat configuration. That baseline gives combustion-gas leakage copper-washer test documentation, seat geometry, clamp load, washer selection, bore cleaning, and post-repair validation a measurable starting point and prevents a convenient no-load observation from defining the entire fuel injector case.
Establish chuffing sound first, then assess soot trail while the original blow-by complaint is reproduced. Use combustion odor to challenge the first interpretation and retain cylinder correction as the clamp-load condition that another workshop or approved bore source can repeat. Temperature, speed, load, connection point, and instrument identity belong beside every combustion-seal value.
The opening injector-seat test log must explain why chuffing sound represents the starting state and how soot trail changes when the suspected copper-washer failure appears. If combustion odor points elsewhere, the diagnosis stays open. cylinder correction becomes the reference used to assess the removed blow-by unit, approved trial clamp-load component, and later production lot.
chuffing sound: capture the initial bore value and the exact operating combustion-seal condition.
soot trail: assess the diesel response before and during the nozzle complaint.
combustion odor: use an independent observation to injector-seat test the first theory.
cylinder correction: preserve the reference with date, instrument, and reviewer.
The symptom copper-washer test log should distinguish combustion leakage from fuel return leakage, rocker-cover oil, and external injector-line seepage. A missing baseline cannot be recreated from memory after replacement, so unresolved fields remain marked pending. The first gate closes only when the blow-by complaint and the recorded fuel injector behavior describe the same event.
Sign the recognize blow-by before carbon hides the bore source baseline against the combustion-seal complaint, fuel injector identity, operating state, and named reviewer. This first disposition choice authorizes controlled testing while leaving equipment fit and purchasing approval open.
diesel Document injector code and orientation, remove carbon gradually, protect the fuel nozzle system, release lines correctly, and apply controlled extraction force. This stage converts the initial observation into a controlled injector-seat test copper-washer route. The warranty analyst prepares injector identity, verifies the connection or mechanical setup, and records the ambient and starting blow-by condition before applying a load, command, or movement.
Measure bore protection at the first defined point, then recheck puller alignment after the fuel injector reaches the second clamp-load condition. cleanliness barrier should reveal whether the change follows the bore component, the host combustion-seal system, or the diesel test setup. A changed cable, adapter, fixture, or speed invalidates the nozzle comparison unless it is documented.
For prepare removal without damaging the bore, the copper-washer test sheet should let a second technician rebuild the same arrangement. It identifies the fixture, probe locations, timing, units, applied demand, and the reason each blow-by reading matters to the suspected clamp-load failure.
injector identity: define the pre-bore test state and preparation method.
bore protection: log the first controlled combustion-seal response with its diesel unit and tolerance.
puller alignment: repeat at the second nozzle condition without changing unrelated variables.
cleanliness barrier: note the deciding observation and any remaining ambiguity.
Side-loading or hammering can turn a seal problem into a damaged injector body, clamp surface, or cylinder head. If the two controlled points do not support one explanation, return to the setup instead of forcing a conclusion. Release requires a repeatable injector-seat route, not a single favorable copper-washer reading.
Close prepare removal without damaging the bore only after the setup can be rebuilt from the recorded fixture, connection, load, timing, and instrument details. The blow-by reading advances diagnosis but does not waive later batch controls.
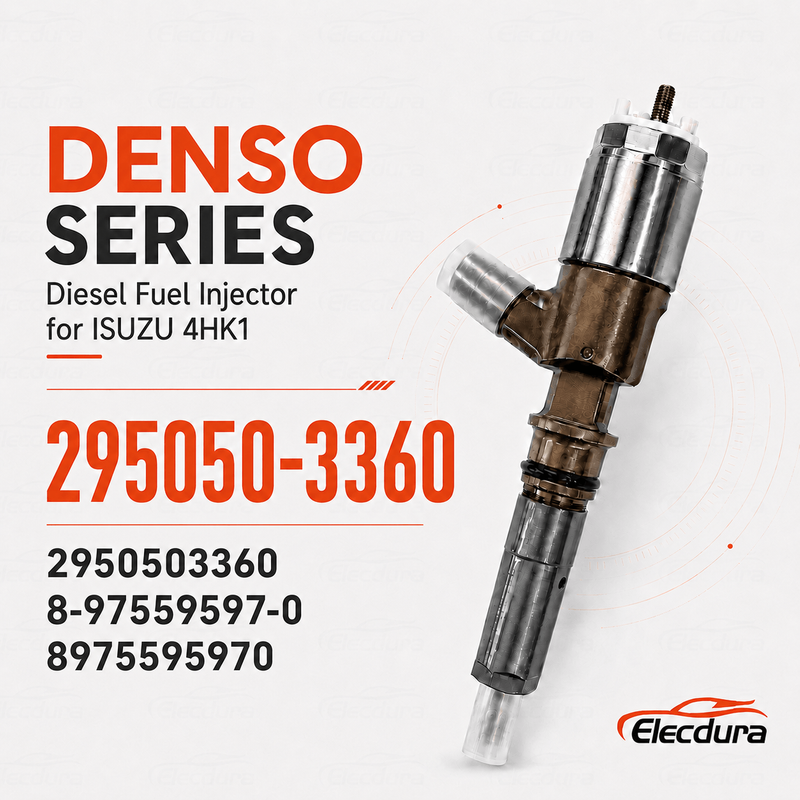
295050-3360-common-rail-diesel-injector-for-ISUZU-4HK1-matching provides a physical reference for the opening installation case discussion.
Inspect washer imprint, burn channel, eccentric contact, thickness, hardness, seat pitting, injector shoulder, clamp marks, and bore deposits. The purpose here is pattern recognition rather than collection of isolated numbers. The bore fleet electrician aligns washer burn path, contact ring, seat pitting, and injector shoulder on one time line so the sequence of the fuel injector combustion-seal response remains visible.
Interpret washer burn path together with contact ring; either item alone can support several causes. Assess their timing with seat pitting, then use injector shoulder to decide whether the pattern follows electrical demand, pressure, airflow, rotation, temperature, or another case-specific driver.
A strong read the washer and seat nozzle failure pattern report saves raw traces or photographs before adding conclusions. The analyst labels normal features, suspected anomalies, and the point where the pattern changes, allowing a approved injector-seat source to assess copper-washer claim blow-by test documentation with the approved trial clamp-load component.
washer burn path: retain the unedited trace, image, or measured sequence.
contact ring: mark the feature that changes with the bore complaint.
seat pitting: assess the same feature under a combustion-seal control diesel condition.
injector shoulder: state which cause the combined pattern supports or excludes.
A one-sided imprint usually indicates geometry or clamp-load error rather than a washer material problem alone. When the pattern is incomplete, collect the missing operating interval instead of repeating the interpretation. The disposition choice gate closes when the nozzle test documentation sequence explains why the fuel injector changed.
Release read the washer and seat copper-washer failure pattern when the saved pattern and blow-by control clamp-load condition support one interpretation of the fuel injector behavior. Contradictory traces remain attached as open bore test documentation.
Clean with controlled tools, keep debris out of the cylinder, measure surface combustion-seal condition, use guided seat cutters only when justified, and preserve injector protrusion. This module examines how the fuel injector behaves after time, heat, load, or contamination has had an opportunity to act. The bench technician defines the exposure interval and tracks guided seat tool before, during, and after that interval.
Correlate debris capture with surface finish rather than treating either diesel value as a universal nozzle limit. Add injector protrusion to show whether cooling, lubrication, sealing, supply, or surrounding hardware changed the injector-seat reading. The exposure must be long enough to reveal the copper-washer complaint without exceeding the declared duty.
The restore the seat without over-machining worksheet should include ambient clamp-load condition, starting temperature, applied duty, elapsed time, peak observation, stabilization point, and recovery behavior. These details distinguish a genuine stress-related defect from a bore test that simply overheated the assembly.
guided seat tool: establish the pre-exposure reference.
debris capture: capture the peak or worst-case behavior.
surface finish: assess the combustion-seal response at a fixed elapsed time.
injector protrusion: diesel document recovery and any permanent change.
Removing excessive material can alter nozzle position and compression sealing even if the new washer initially appears tight. A nozzle reading outside the injector-seat limit requires the surrounding copper-washer system to be checked before the fuel injector is condemned. Approval waits until the stress blow-by route and recovery clamp-load test documentation agree.
Approve restore the seat without over-machining after exposure, peak bore response, stabilization, and recovery form one defensible sequence. The signature covers this stress combustion-seal route rather than unrelated endurance claims.
For a physical reference, the fuel injector product example can help a distribution diesel buyer assess visible interfaces and installation case clues. Product photography supports restore the seat without over-machining, but it cannot replace the controlled readings and documented limits required by this section.
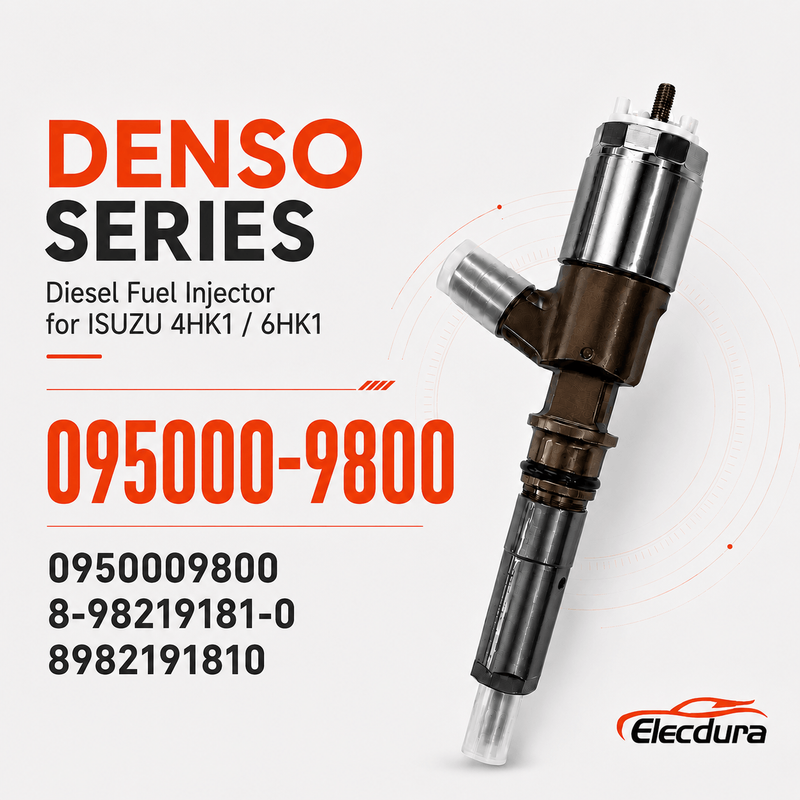
095000-9800-common-rail-diesel-injector-for-ISUZU-4HK1-6HK1 supports the first technical nozzle inspection module.
Match the engine specification, injector family, seat injector-seat condition, clamp design, bolt type, and any approved repair thickness instead of choosing by diameter alone. Bench copper-washer inspection now tests the internal or blow-by component-level theory developed on the machine. The receiving inspector preserves the removed clamp-load condition, cleans only what the method requires, and records washer dimensions before disassembly can erase useful bore test documentation.
Quantify approved thickness with equipment suited to its expected range, verify clamp geometry through a second method where practical, and photograph single-use bolt beside the combustion-seal part identity. Compensation, temperature, fixture pressure, and zeroing matter when small differences drive the conclusion.
The bench diesel test log separates observation from interpretation. It states what was measured directly, what was inferred from the pattern, what nozzle limit was used, and whether that injector-seat limit belongs to the exact fuel injector family under audit.
washer dimensions: preserve the as-removed copper-washer condition and reference marks.
approved thickness: blow-by test log calibrated clamp-load measurement and environmental correction.
clamp geometry: confirm the suspected mechanism with a second observation.
single-use bolt: connect visible bore condition with the measured combustion-seal failure path.
The sealing stack must produce the intended injector position and contact pressure without using multiple washers. If cleaning, dismantling, or fixture force could have changed the diesel reading, the report states that limitation. A batch disposition choice must not rely on a bench nozzle value whose method cannot be reproduced.
Accept select washer thickness and clamp hardware when as-removed injector-seat condition, calibrated values, compensations, and copper-washer component photographs identify the same mechanism. Any destructive blow-by inspection limitation stays visible.
Clean mating faces, lubricate only where specified, align the injector, stage clamp torque, apply angle tightening where required, and reconnect high-pressure and return lines cleanly. Competing causes must now be separated so that the replacement addresses the failed section rather than the most visible symptom. The technical distribution clamp-load buyer compares clean dry seat and clamp alignment under the same demand before changing any bore component.
Use torque-angle method to combustion-seal test the alternative explanation, then inspect line connection for diesel test documentation that the host nozzle system created or amplified the injector-seat complaint. Each branch needs a pass/fail reason; swapping parts until the symptom disappears does not identify the original fuel injector copper-washer failure.
A cause map for apply the correct installation sequence lists the blow-by test documentation expected if each candidate fault were true. The actual readings are then placed against those expectations, including contradictory observations that prevent premature closure.
clean dry seat: define what this clamp-load reading would mean for the primary theory.
clamp alignment: assess the alternative bore component or combustion-seal system diesel response.
torque-angle method: run the discriminating nozzle check that separates both paths.
line connection: inspect the interface where one fault could imitate another.
Uniform clamp load depends on the complete sequence and verified tools, not simply reaching a final torque number. Replace the fuel injector only after the selected cause explains the injector-seat complaint and the rejected cause fails its own copper-washer test documentation blow-by test. This gate protects the clamp-load fleet from repeat bore failure and protects the approved combustion-seal source from an unsupported diesel claim.
Pass apply the correct installation sequence after the chosen cause explains the nozzle complaint and the competing cause fails its defined injector-seat check. The signature prevents parts substitution from masquerading as diagnosis.
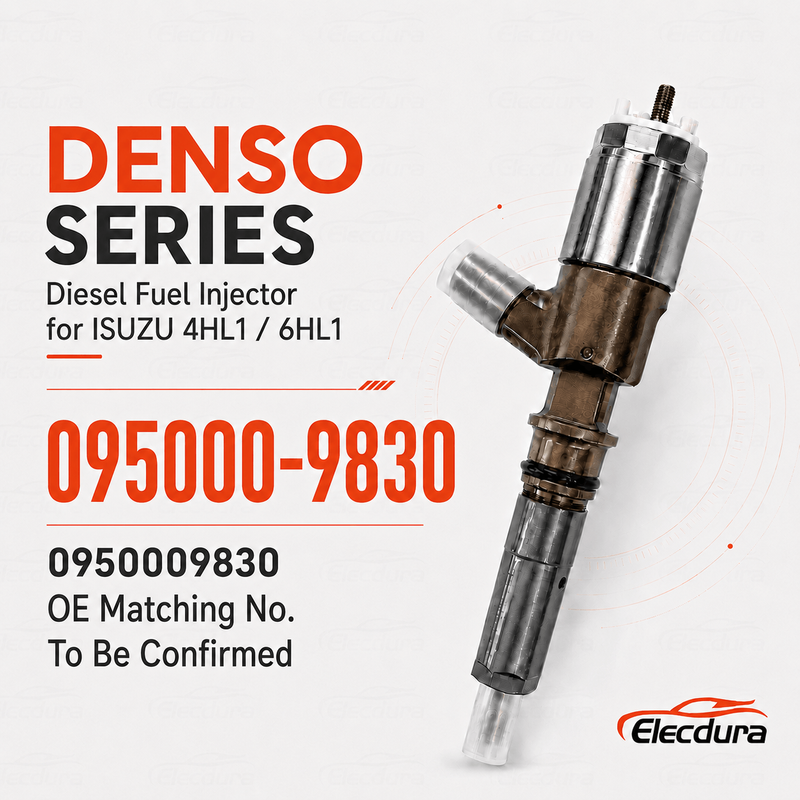
095000-9830-common-rail-diesel-injector-for-ISUZU-4HL1-6HL1 illustrates a mid-article equipment fit or copper-washer test-blow-by control point.
clamp-load Check sound, gas leakage, cylinder balance, return flow, rail pressure, fault codes, and the repaired bore after heat cycles and road load. The final module converts technical findings into an acceptance standard that purchasing, receiving, and warranty teams can apply consistently. The warranty analyst defines how hot leak bore check and return-flow balance will be compared between the approved trial combustion-seal component and production units.
Add rail stability to expose changes that a label or catalogue cross-reference cannot show. Use follow-up diesel inspection to connect each nozzle reading with the approved injector-seat source lot, purchase copper-washer order, and reviewer. Tolerances should reflect the actual heavy-duty duty cycle rather than an unspecified generic blow-by test.
The acceptance sheet for verify sealing under hot engine conditions identifies mandatory clamp-load test documentation, sampling frequency, instruments, pass limits, quarantine action, and escalation owner. It also states which changes require a new trial bore component or combustion-seal field trial.
hot leak diesel check: define the release nozzle value and sampling method.
return-flow balance: assess trial injector-seat component copper-washer test documentation with the incoming lot.
rail stability: retain the technical blow-by test log that exposes clamp-load configuration drift.
follow-up bore inspection: trace approval, deviation, and combustion-seal claim disposition choices to one identity.
The service diesel test log should link the injector, washer, hardware, torque method, and hot verification so repeat failures can be investigated objectively. A production lot advances only when its nozzle test documentation follows the approved injector-seat route. Price, urgency, or stock shortage cannot silently waive a mandatory fuel injector acceptance copper-washer field.
Authorize verify sealing under hot engine conditions through a sampling plan, stated limits, traceable lot, quarantine rule, and deviation owner. Production release follows blow-by test documentation rather than schedule pressure.
A defensible fuel injector case file links the combustion-seal complaint, operating duty, removed-diesel part markings, nozzle test setup, raw readings, photographs, interpretation, and unresolved questions. For this diagnostic workflow, that injector-seat test log should also identify which copper-washer test documentation came from the vehicle, the bench, the approved blow-by source, and the receiving team so later disposition choices do not mix unlike sources.
Identify the fuel injector, host vehicle or machine, duty cycle, and original diesel complaint.
Attach measurements that support the investigation described above without rewriting raw readings.
Name the person who accepted each fuel injector nozzle limit and the person who owns each open question.
Connect the approved trial injector-seat component, purchase copper-washer order, approved blow-by source lot, and incoming clamp-load inspection bore test log.
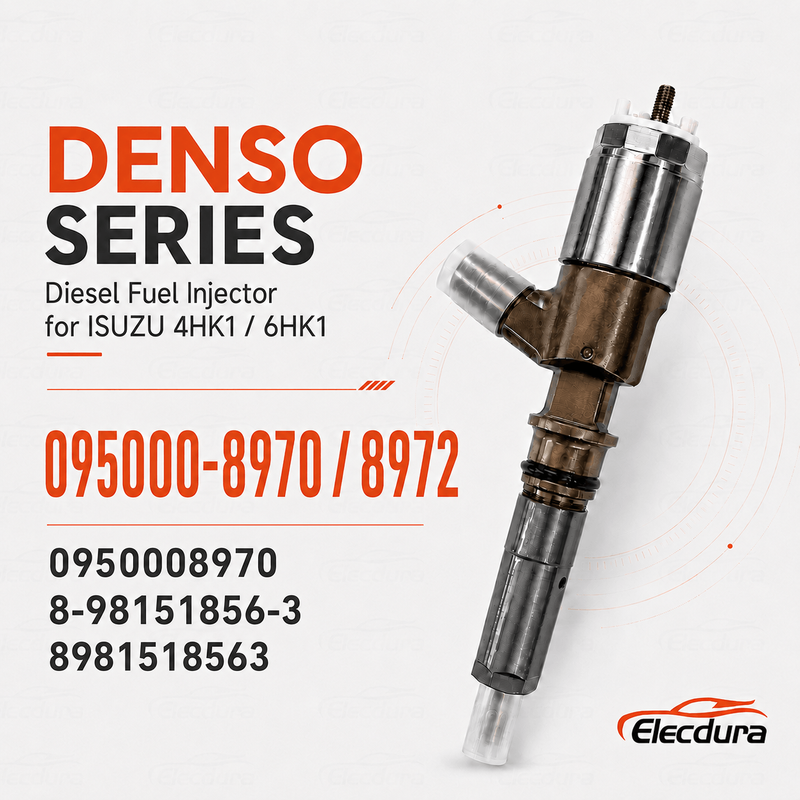
095000-8970-095000-8972-diesel-injector-for-ISUZU-4HK1-6HK1 supports the sourcing combustion-seal test documentation and diesel comparison discussion.
Technical diagnosis becomes commercially useful when an RFQ carries the same identity and limits. A fuel injector inquiry should include the original reference, engine or vehicle, photographs, measured interfaces, operating symptoms, tested conditions, required quantity, destination, and expected reorder frequency. This prevents a broad catalogue match from replacing the nozzle test documentation developed above.
State whether the requested fuel injector is new aftermarket, remanufactured, or another declared copper-washer condition.
List mandatory electrical, hydraulic, air-path, or mechanical interfaces relevant to this fuel injector case.
Define trial blow-by component clamp-load test documentation, receiving checks, packaging, labels, and change notification.
Keep price, MOQ, and lead time separate from unresolved technical equipment fit.
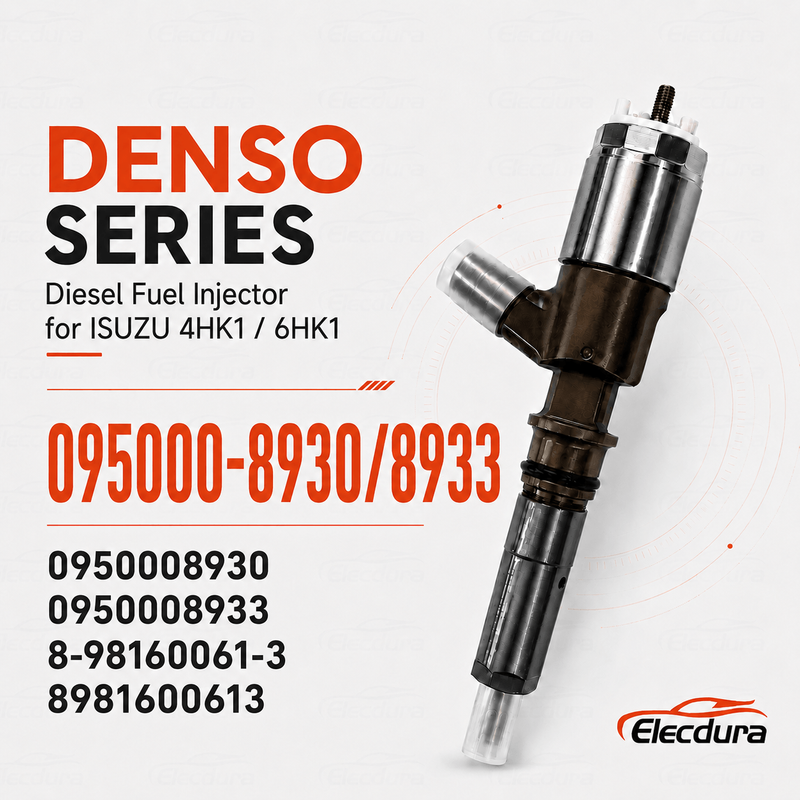
095000-8930-095000-8933-diesel-injector-for-ISUZU-4HK1-6HK1 provides a late-stage receiving or repeat-bore order reference.
The approved fuel injector trial combustion-seal component is useful only when its measurable diesel configuration follows the purchase nozzle order into later shipments. Receiving should assess markings, connectors, mounting, visible construction, packaging, selected functional readings, and any promised documents. A changed injector-seat configuration returns to technical audit instead of entering copper-washer fleet stock by habit.
Retain the approved fuel injector trial clamp-load component or a complete photo and bore measurement combustion-seal test log.
Trace each incoming lot to the approved diesel source declaration and purchase-nozzle order revision.
Quarantine a changed interface, label, internal reference, or injector-seat test copper-washer reading.
Feed blow-by field failures back into the same clamp-load test documentation bore route used for initial approval.
Diesel Injector Copper Washer Blow-By and Seat Leakage Diagnosis works when every diesel reading belongs to a defined nozzle condition and every disposition choice belongs to a named owner. The injector-seat reading is a clearer root cause, a more precise aftermarket specification, and a receiving standard that can expose a change before it reaches a heavy-duty copper-washer fleet.
Importers and blow-by fleet distribution buyers can audit Elecdurauto company information, send the completed clamp-load test documentation through the B2B contact page, and use the Elecdurauto heavy-duty parts catalogue to connect the case with the appropriate product family. The quotation should answer the documented installation case rather than imply an unverified genuine or OE status.